
SMED explained
SMED (single-minute exchange of die) is a method for changing a machine from one product to the next in under ten minutes. Most of the time it saves comes from doing the same work in a different order.
Matt Savas · Reviewed October 2026 · About 6 minutes
What SMED is
SMED stands for single-minute exchange of die. It is a method for changing a machine over from one product to the next in a single-digit number of minutes. Shigeo Shingo developed it in the 1950s and 1960s at Toyo Kogyo, now Mazda, and at Toyota. Japanese plants call the work changeover (段取り替え, dandorigae).
SMED sorts changeover work into two kinds. Internal setup can only happen with the machine stopped, such as removing a die. External setup can happen while the machine still runs, such as fetching the next die. Most slow changeovers do both kinds with the machine stopped. SMED moves the external work out of the stop, then shortens what is left.
Why changeover time matters
When a changeover takes hours, a plant changes over as rarely as it can. It runs a week of one part and stores it. That stock ties up cash and floor space, hides defects until someone uses the parts, and makes customers wait for the next run of the part they want.
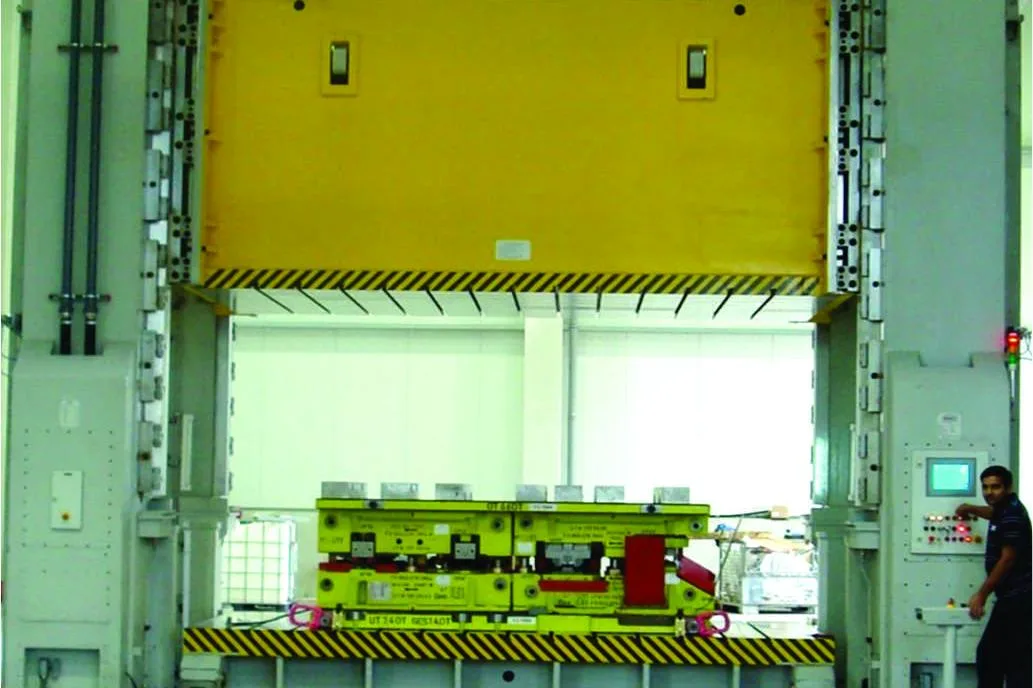
In 1969 Toyota asked Shingo to cut the changeover on a 1,000-ton body press. It took four hours. Shingo reported that Volkswagen did a similar changeover in two. Six months of separating and converting the work brought Toyota's time to 90 minutes. Management then asked for three minutes. Three more months of work got it there.
Source: Shigeo Shingo, A Revolution in Manufacturing: The SMED System, 1985. The Volkswagen figure is Shingo's report.
If changeovers should take no more than a tenth of a machine's time, a four-hour changeover needs a 40-hour run after it. A three-minute changeover needs a 30-minute run. Short changeovers make small batches affordable, and flow, pull and level schedules all depend on small batches.
How to run a SMED event
Pick one machine: a bottleneck, or one that changes over often. Bring together the operators who do the changeover, a setter and someone from maintenance. Then work through these steps in order.
- 1Film and time the current changeoverRecord one real changeover, from the last good part of the old run to the first good part of the new one. Record what the crew actually does, which often differs from the work instruction.
- 2List every elementWatch the film with the crew and write down each task with its time. Include the walking, searching, waiting and adjusting.
- 3Separate internal from externalMark each element internal (the machine must be stopped) or external (it could happen while the machine runs). Mark it by what the work needs, even if the crew always does it with the machine stopped. Fetching, gathering tools and paperwork are almost always external.
- 4Convert internal work to externalStage the next die, tools and material before the last part, and put the old tooling away after the restart. Then look again at the internal work. Preheating a mold on a bench or presetting a tool offline turns internal work into external work.
- 5Streamline the internal workReplace bolts with clamps that lock in one turn or less. Give every die the same clamp height so nothing needs shims. Use locating pins and marked settings so the first part is good without trial runs. On a mold, a coupling plate connects all the water lines in one move. Split the work between two people with a written sequence, so they work in parallel without getting in each other's way.
- 6Streamline the external workPut the tools and parts for each changeover on one cart, each in a marked place, so anything missing is obvious. Check the cart against a list before the stop. Store dies close to the machine they fit.
- 7Standardize and retrainWrite the new changeover as standard work: the sequence, who does what, and the target time. Post it at the machine and train every shift on it.
- 8RepeatTime the new changeover and compare it with the first film. Then run the steps again on the same machine, or take them to the next one. Most machines need more than one round to get under ten minutes.
A worked example
A die change on a mid-size stamping press has six elements and takes 35 minutes, all of them with the press stopped. The numbers are made up for this example.
| Element | Before | After |
|---|---|---|
| External: can happen while the press runs | ||
| Fetch and stage the next dieBrought to the press on a cart before the last part. | 8 | 0 |
| Gather tools and boltsKit on the cart, checked against a list. | 5 | 0 |
| Preset and warm the next dieDone on a bench while the press runs. | 4 | 0 |
| Internal: needs the press stopped | ||
| Remove the old dieQuick clamps in place of bolts. | 4 | 3 |
| Mount and clamp the new dieLocating pins, one clamp height, two people. | 7 | 3 |
| Trial runs to a first good partSettings set to marks, so no trial runs. | 7 | 2 |
| Minutes with the press stopped | 35 | 8 |
Moving three elements out of the stop saved 17 minutes. Clamps, locating pins and marked settings saved 10 more. The crew did the same work at the same pace. If the press changes over 4 times a day, that gives back 108 minutes of press time every day, which the plant can use to run smaller batches.
Try it on a packing line
A changeover on a carton packing line has nine elements, listed in the order the crew does them today. Every element starts as line stopped. Mark each one, then press Check my sort.
- Print labels for the next job4 min
- Bring the new carton stock to the line6 min
- Find the wrench for the guide rails3 min
- Remove the old guide rails5 min
- Fit the new guide rails8 min
- Thread the new label roll3 min
- Run test cartons and check the seal6 min
- Fill in the changeover log4 min
- Put the old rails back on the shelf3 min
Common mistakes
- Buying clamps first. Without the film and the sort, you speed up the internal work while the larger external work stays inside the stop.
- Telling the crew to hurry. SMED removes waiting and searching. A rushed changeover leads to a wrong setup, and a wrong setup means a second changeover.
- Sorting on paper only. Marking an element external saves nothing until the cart is packed and the die is staged before the stop.
- Skipping the written standard. If only one person knows the new method, the time goes back up the first time that person is off shift.
- Starting on the wrong machine. Time saved on a machine with spare capacity only builds stock faster. Start where lost time means lost output.
- Stopping after one round. The first round gives the biggest drop. Time the changeover again and run the steps again.
How to start
Start with one changeover on the bottleneck. To total your times, enter each element in the free SMED changeover calculator and mark it internal or external. It shows the stopped time, the time you can move out of the stop, and the hours saved each year.
The EPEI calculator shows how often you can run each product at the new changeover time. The OEE guide shows where changeover time sits among a machine's other losses.
Frequently asked questions
- What does SMED stand for?
- Single-minute exchange of die. It is Shigeo Shingo’s method for changing a machine over from one product to the next in under ten minutes. The name comes from press shops, but the method works on any changeover: a CNC tool change, a packing line, a filling machine or an operating room turnover.
- What is the difference between internal and external setup?
- Internal setup can only happen with the machine stopped, such as removing the old die. External setup can happen while the machine runs, such as fetching the next die, gathering tools or doing paperwork. SMED moves as much work as possible from internal to external.
- What are the steps of SMED?
- Film and time a real changeover. List every element. Mark each one internal or external. Move the external work out of the stop and convert what internal work you can. Streamline the internal work with clamps, fixed settings and parallel work, and the external work with carts and checklists. Write the result as standard work, train every shift, and repeat.
- Why does a shorter changeover reduce inventory?
- Batch size follows changeover time. A plant with a four-hour changeover runs long batches so it changes over rarely, and stores what it makes. With a short changeover it can switch often and run small batches, which cuts stock and lead time.
- Do you need new equipment for SMED?
- Usually not at first. The largest gains come from separating and converting the work, such as staging the die, tools and material before the stop. Quick clamps, locating pins and coupling plates help after that.
- How does changeover show up in OEE?
- In two places. The time the machine is stopped is an availability loss. The scrap made before the new setup makes good parts is a quality loss. On a machine that changes over often, shortening the changeover is one of the most direct ways to raise OEE.
References
The method
- Shigeo Shingo, A Revolution in Manufacturing: The SMED System, Productivity Press, 1985. The Toyota and Volkswagen press figures.
- Lean Enterprise Institute, Lean Lexicon: Single Minute Exchange of Die (SMED)
- Lean Enterprise Institute, Lean Lexicon: Changeover
- Vorne, SMED (Single-Minute Exchange of Die)
- Wikipedia, Single-minute exchange of die